Loading page
Black oxide
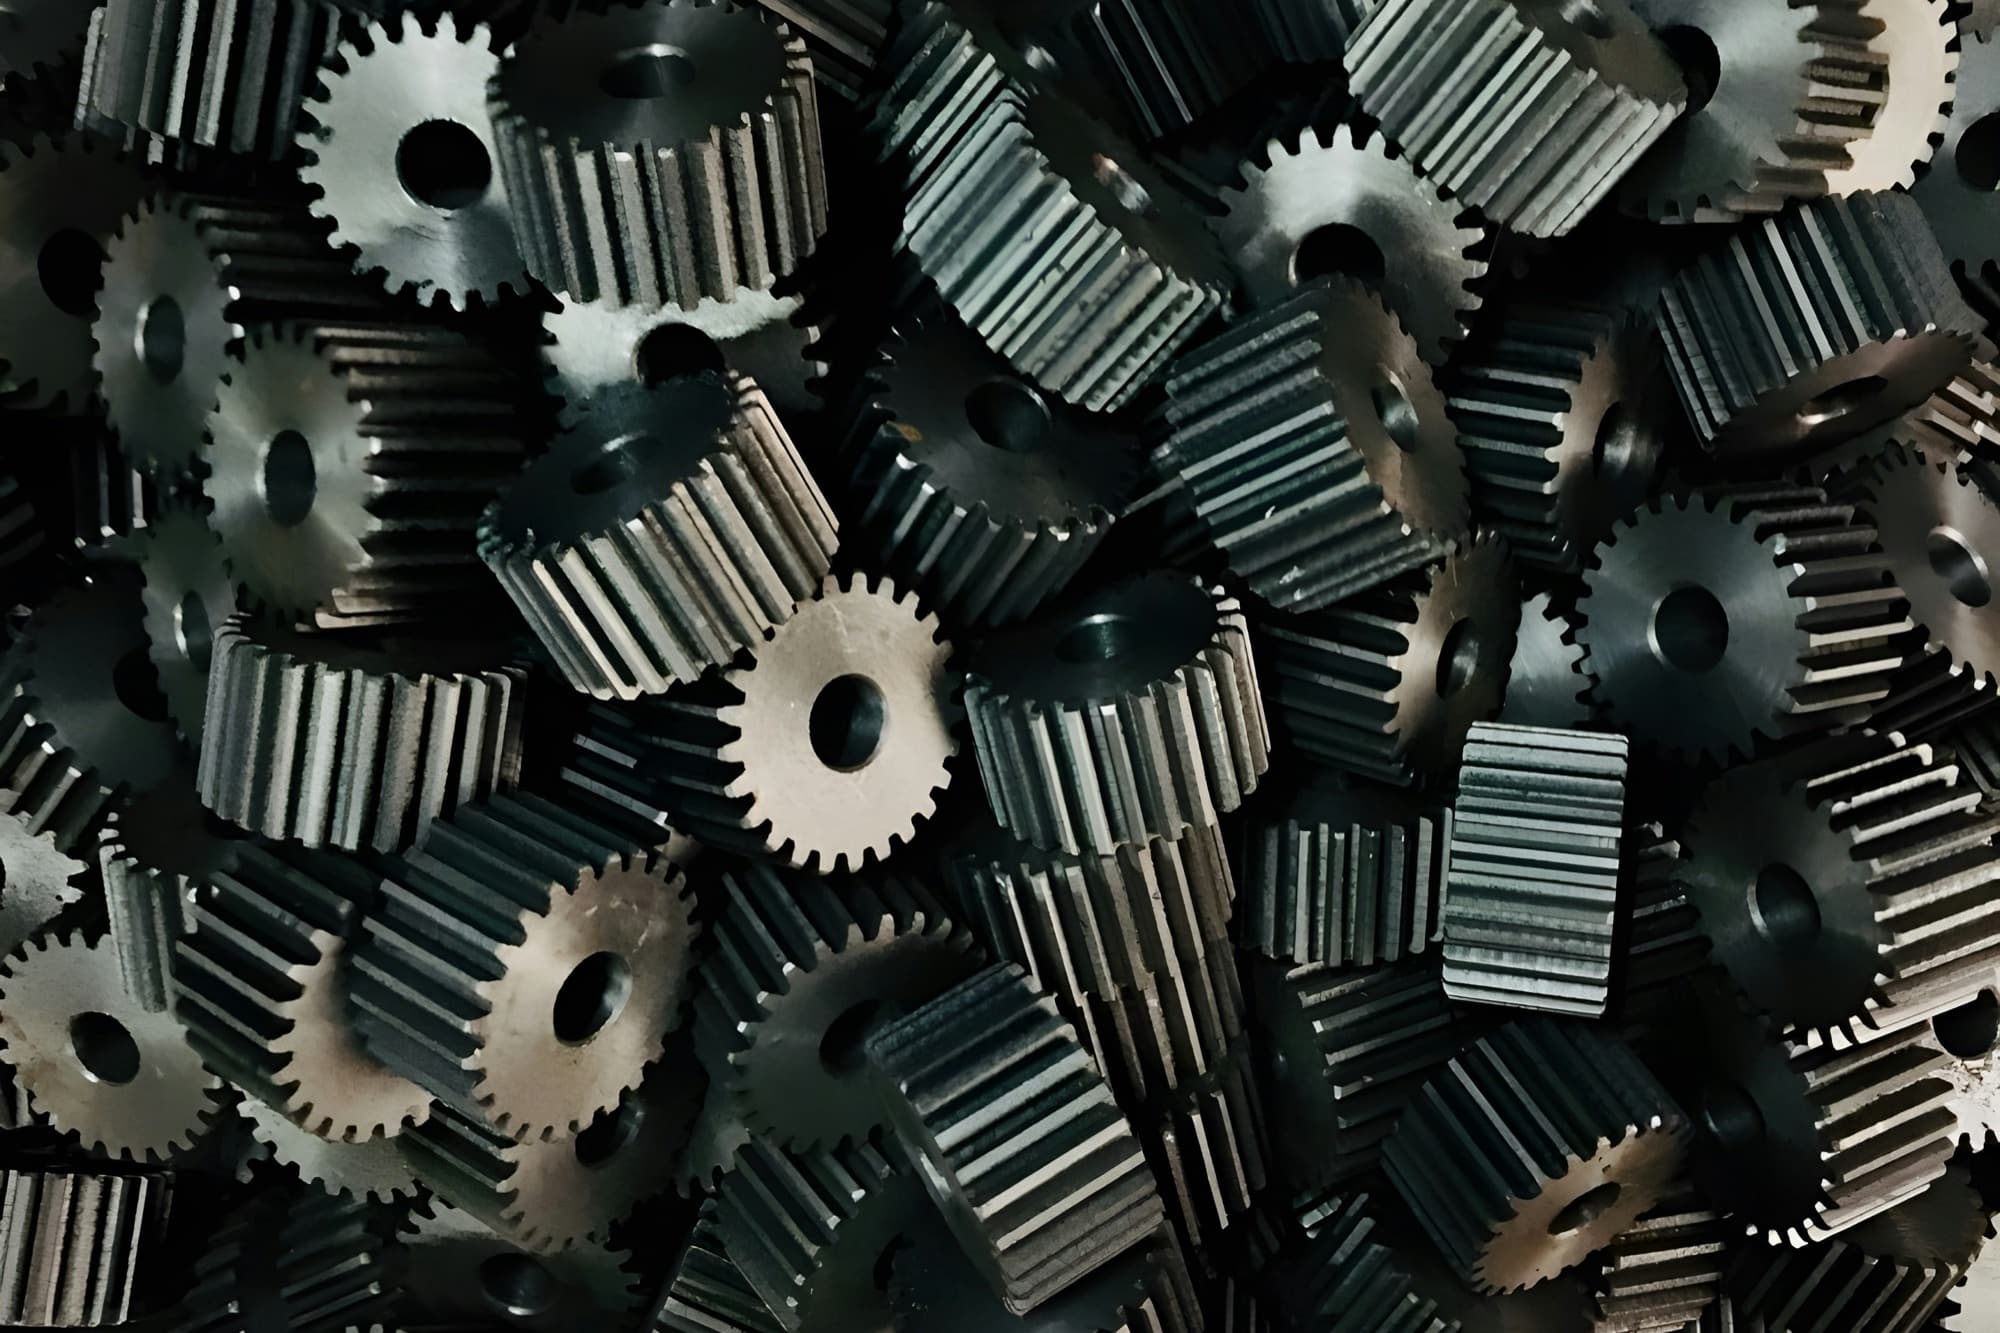
Black oxide is a conversion coating that turns the surface of steel into black magnetite (Fe3O4) in a hot alkaline salt bath at about 285 °F (141 °C). The layer is about 0.00004 in (1 µm), so it adds no meaningful thickness and suits threads and precision parts. On its own it gives little corrosion protection; a supplemental oil or wax provides mild indoor protection.
- Applies to
- Carbon and alloy steels, tool steels, stainless steels (with stainless-specific processes) and sealed powder metal parts
- Adds
- 3 days
- Cost
- Low

Colors
- Black (oiled)
- Black (dry)
Specs
| Thickness | About 0.00002–0.00004 in (0.5–1 µm); no dimensional change |
|---|---|
| Process | Hot alkaline oxidizing salts at about 285 °F (141 °C) |
| Supplemental coating | Rust-preventive oil, wax or dry lacquer |
| Corrosion resistance | Low; indoor use unless oiled and handled carefully |
| Hydrogen embrittlement | Negligible |
| Appearance | Uniform matte to semi-gloss black |
Call out on the drawing
- MIL-DTL-13924 Class 1 (carbon and low-alloy steel); Classes 2–4 for stainless
- AMS 2485 (black oxide coating)
- MIL-PRF-16173 (supplemental corrosion preventive, when specified)







Questions
Does black oxide prevent rust?
Only mildly, and mostly because of the oil or wax applied afterward. Oiled black oxide is fine indoors and on parts that stay lubricated. For outdoor or humid service, use zinc plating, zinc-nickel or black e-coat instead.
Does black oxide change dimensions?
No meaningful change. The converted layer is about 1 µm, so threads, bores and gauged features stay in tolerance. That is its main advantage over plating.
Can stainless steel be black oxided?
Yes, with processes designed for stainless, covered by MIL-DTL-13924 Classes 2–4. The finish is decorative and reduces glare; it adds no corrosion resistance beyond the stainless itself.
Hot vs cold black oxide?
Hot black oxide converts the surface to magnetite and is durable. Room-temperature cold blackening deposits a copper-selenium compound that is less abrasion resistant and less consistent. Use hot black oxide for production parts.


Price it with this finish.
The builder adds lot charges, per-part cost and lead time for the finish you pick.