Injection molding design review: resin and DFM checklist
SSG MFG engineering6 min readInjection molding
What should an injection molding design review cover before cutting steel?
An injection molding design review confirms, before the mold is cut, that the resin grade meets the part's temperature, chemical, and agency requirements and that the geometry can be molded: uniform walls, adequate draft, ribs under 60% of the wall, planned gate and knit line locations, an undercut strategy, and tolerances matched to the resin's shrink. Changes after steel is cut cost far more.

Why review an injection molded part before cutting steel?
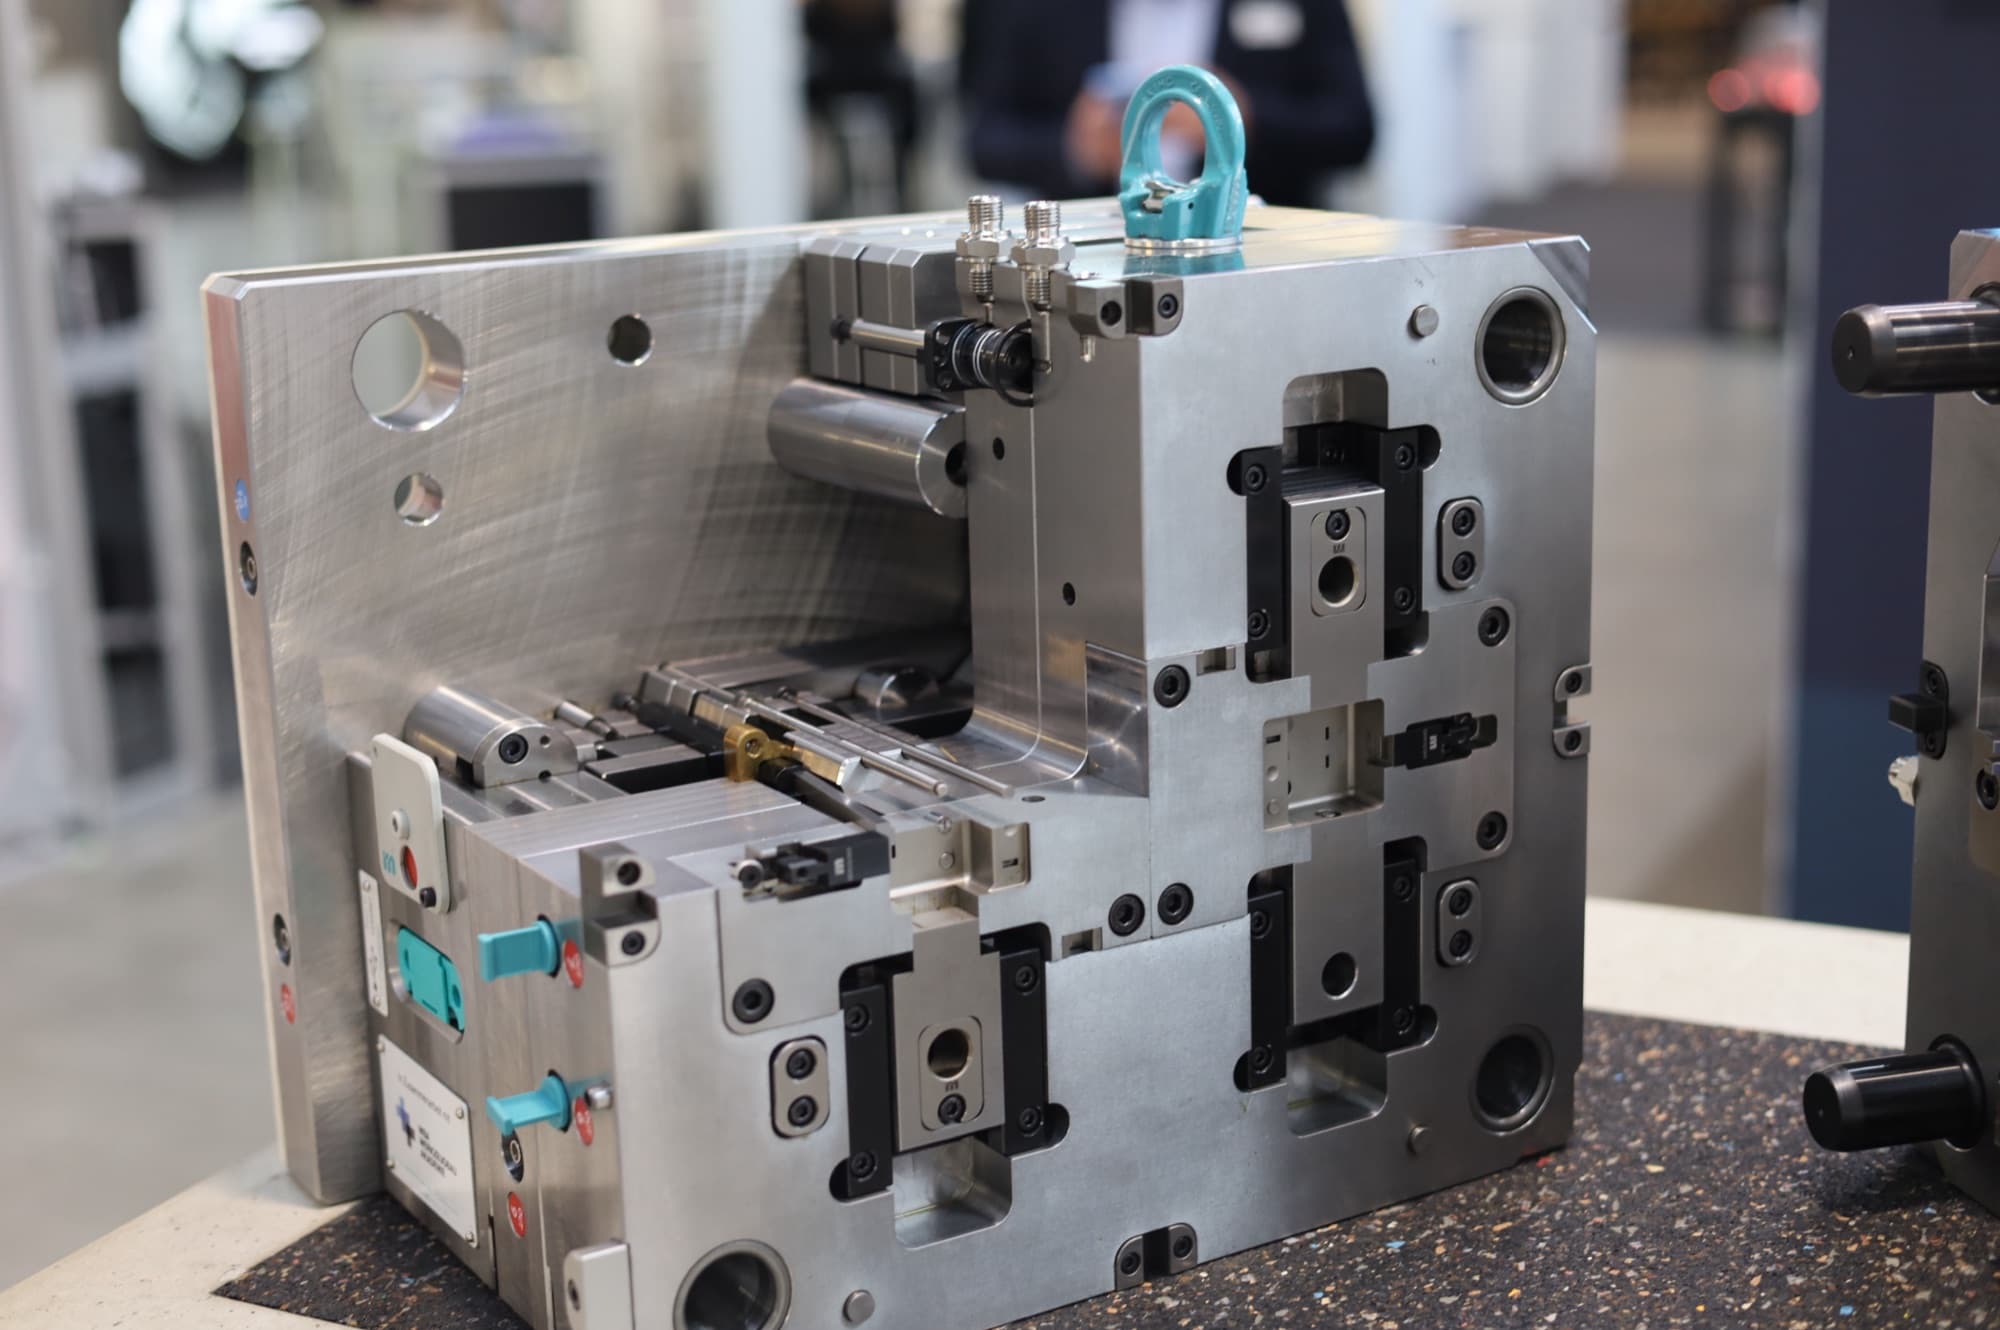
A production mold is a machined steel tool that often takes 6–12 weeks to build and is usually the largest single cost in a molded part's launch. Once the cavity is cut, geometry changes mean welding, recutting, or replacing inserts, and each change adds weeks. A structured review catches most of those changes while they are still edits to a CAD file.
Toolmakers also cut critical features steel-safe, leaving extra steel so a dimension can be corrected by removing metal after the first shots. Removing steel is fast and inexpensive. Adding it back by welding is slow, costly, and can leave witness marks on the part.
How do you choose the right resin for a molded part?
Start with the environment, not the material used on the last program. List the maximum and minimum temperatures, the chemicals the part touches, UV exposure, loads, and agency requirements. Then pick the lowest-cost resin that passes all of them with margin.
- Temperature: heat deflection temperature (ASTM D648) for short-term loads, and UL 746B relative thermal index for long-term use.
- Flammability: the UL 94 rating required (HB, V-2, V-1, V-0, or 5VA) at the part's actual wall thickness.
- Mechanical: tensile strength (ASTM D638), flexural modulus (ASTM D790), and notched Izod impact (ASTM D256).
- Chemical and UV exposure: cleaners, oils, fuels, and sunlight; specify UV-stabilized grades for outdoor parts.
- Regulatory: FDA 21 CFR 177 for food contact, RoHS and REACH, and any customer material lists.
- Appearance: color, gloss, texture, and whether a custom color match is required.
| Resin | HDT at 264 psi (1.8 MPa) | Strengths | Watch-outs |
|---|---|---|---|
| ABS | 185–210°F (85–99°C) | Low cost, good impact, easy to mold and decorate | Poor UV and solvent resistance |
| Polycarbonate | 265–285°F (129–140°C) | Clear, very tough, dimensionally stable | Notch sensitive; attacked by some solvents |
| PC/ABS | 205–240°F (96–116°C) | PC toughness with easier molding | Moderate chemical resistance |
| Polypropylene | 120–140°F (49–60°C) | Low cost, chemical resistant, living hinges | High shrink, warp, low stiffness |
| Acetal (POM) | 220–260°F (104–127°C) | Low friction, wear resistant, stable | Hard to bond or paint; attacked by acids |
| Nylon 66, 30% glass | 470–490°F (243–254°C) | Stiff, strong, heat resistant | Absorbs moisture; anisotropic warp |
| PBT, 30% glass | 400–420°F (204–216°C) | Stable, good electrical properties | Warps; notch sensitive |
What does the geometry review check?
- Nominal wall and variation: walls within about 10–15% of nominal, with gradual transitions.
- Draft on every face parallel to the pull: 1° by default, more on textured faces and cores.
- Ribs and bosses: rib thickness 40–60% of the wall, bosses cored to the base.
- Corners: inside radius at least half the wall; no sharp inside corners.
- Parting line: location, cosmetic impact, and flash risk.
- Undercuts: each one resolved by pass-through coring, a side action, a lifter, or a redesign.
- Gate and knit lines: gate location agreed, and knit lines kept off load paths and cosmetic faces.
- Ejection: room for ejector pins on non-cosmetic faces, with acceptable witness marks.
- Thin steel: narrow, tall mold features between close walls or holes, which run hot and break.
- Text and logos: raised lettering on the part is cut into the mold and costs less than recessed lettering.
When is a mold flow analysis worth it?
Mold flow simulation predicts how the cavity fills, where knit lines and air traps form, the pressure needed to fill, and how the part warps as it cools. It costs far less than a round of steel changes. Run it for cosmetic parts, thin walls, long flow lengths, glass-filled resins, and multi-cavity or family tools.
- Fill time and fill pressure compared with the press capacity quoted.
- Weld line and air trap locations overlaid on the part.
- Gate freeze time, which limits how well thick areas can be packed.
- Warp prediction, with fiber orientation for filled resins.
How do you set tolerances for molded plastic parts?
Tie each tolerance to a function, and check it against the resin's shrink and the part's size. The Plastics Industry Association (formerly SPI) publishes commercial and fine tolerance charts by resin, and ISO 20457 defines tolerance groups for molded parts.
- Use commercial tolerances, about ±0.005 in (±0.13 mm) on the first inch, as the default.
- Reserve fine tolerances, about ±0.002 in (±0.05 mm), for mating features, and expect added cost.
- Loosen tolerances on high-shrink resins such as PP, HDPE, POM, and unfilled nylon.
- Define datums the way the part will be fixtured and inspected, and call flatness only where it matters.
- For critical dimensions, ask for a capability study by cavity; Cpk ≥ 1.33 is a common target.
What should the injection molding RFQ package include?
- 3D model in STEP format and a 2D drawing with critical-to-function dimensions marked.
- Resin grade, color, and any equivalents allowed.
- Estimated annual usage (EAU), release quantities, and expected program life.
- Cosmetic requirements: SPI finish or texture callout, and which faces are Class A.
- Cavitation or cycle expectations, if known, and whether a hot runner is wanted.
- Approval requirements: first article inspection, PPAP level, or capability studies.
- Secondary operations: inserts, pad printing, ultrasonic welding, assembly, and packaging.
What happens at T1 sampling?
T1 is the first trial of the finished mold. The molder establishes a process window, measures parts, and reports dimensions against the drawing. Expect a round of steel-safe adjustments before approval; that is normal, and it is why critical features are left steel-safe.
Approval usually ends with a first article inspection report, or a PPAP submission on automotive programs, and a documented process sheet. Once parts are approved, hold the molder to that process and require notice before any change to resin, press, or plant.
How do you get a molded part reviewed and quoted?
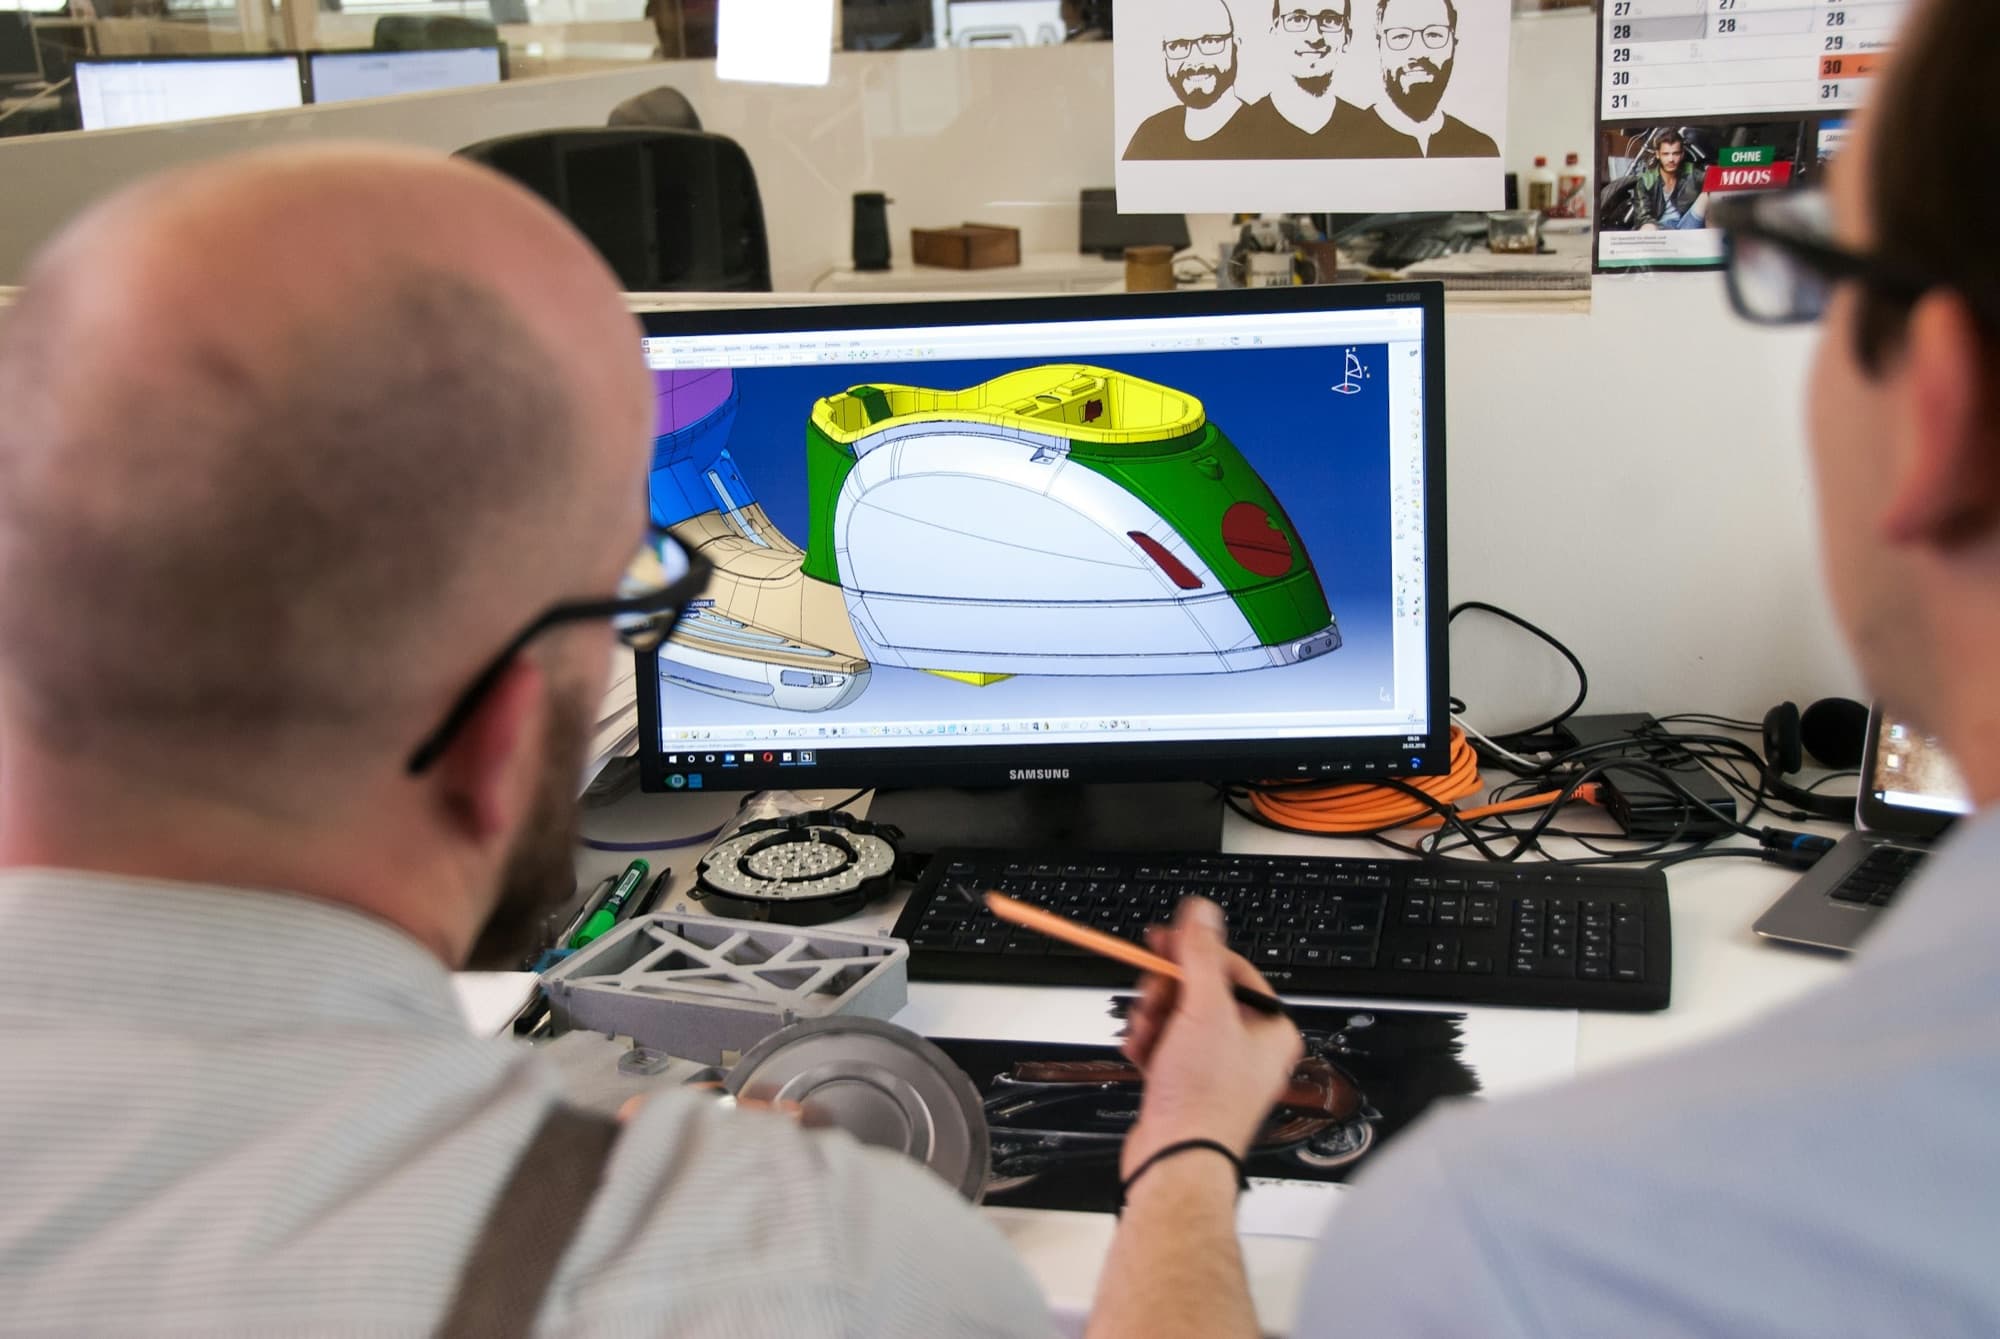
Upload a STEP file or configure the part in the SSG builder at /build for an instant budgetary estimate and an automated DFM check on walls, draft, and undercuts. An SSG rep then routes the RFQ to principals matched to the resin, part size, and volume, and returns firm quotes along with each molder's own DFM comments.